Why Hydroxyl Functionality Matters in Liquid Polybutadiene
Liquid polybutadiene is often selected as a reactive component in polyurethane formulations because its hydroxyl groups allow the polymer to participate directly in urethane formation. But the number and position of those hydroxyl groups can change how the material contributes to the final polyurethane structure.
That distinction becomes particularly important when comparing mono-OH vs di-OH liquid polybutadiene. A mono-hydroxyl material and a di-hydroxyl material may both contain a polybutadiene backbone, yet they do not provide the same level of reactive connectivity during polyurethane formation.
The difference is not simply a matter of choosing one material for flexibility and the other for strength. A more useful way to evaluate the two is to look at the relationship between hydroxyl functionality, OH equivalent weight, molecular weight, NCO/OH ratio, viscosity, and network formation.
For formulators, this matters because changing from one type of liquid polybutadiene to another can alter the amount of isocyanate required, curing behavior, molecular architecture, and ultimately properties such as elongation, hardness, modulus and resilience.
Mono-OH and Di-OH Liquid Polybutadiene Are Used Differently
Mono-OH Liquid Polybutadiene
Mono-OH liquid polybutadiene contains one primary hydroxyl functionality per polymer chain. Because only one hydroxyl group is available for urethane reaction, its contribution to polyurethane network formation differs fundamentally from that of a difunctional polyol.
In a formulation, a mono-hydroxyl polybutadiene can act more like a reactive end-group-bearing modifier or chain-end component. Its effect depends strongly on molecular weight and the amount used. Increasing its concentration does not automatically produce the same type of molecular connectivity as adding a di-OH polyol.
This makes mono-OH materials useful when the formulation needs to introduce a polybutadiene segment while maintaining tighter control over how that segment participates in the growing polyurethane structure.
For applications where a mono-hydroxyl liquid polybutadiene is being considered, the OH value should be checked together with molecular weight rather than treated as an isolated specification. Two products with similar viscosity may still have significantly different reactive behavior if their hydroxyl functionality and molecular-weight distributions differ.
Di-OH Liquid Polybutadiene
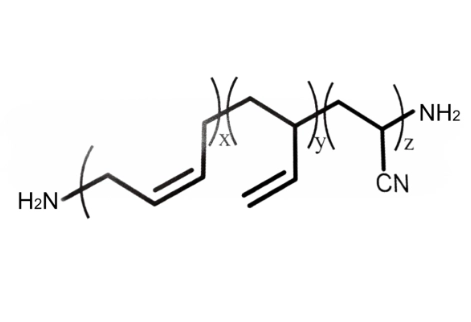
Di-OH liquid polybutadiene contains two hydroxyl functionalities and can therefore react at both ends of the polymer chain. This gives it a more direct role in polyurethane chain growth and network development.
Conventional hydroxyl-terminated polybutadiene is commonly used as a reactive polyol in polyurethane systems for this reason. Its two reactive ends allow the polybutadiene chain to become part of the polyurethane backbone rather than behaving primarily as a terminal modifier.
For formulations based on HTPB, the hydroxyl-terminated polybutadiene grade, OH value, molecular weight and functionality all need to be considered together when determining the required isocyanate level.
The practical advantage of a di-OH structure is not that it is inherently “better.” Its main difference is reactive connectivity. That connectivity can be valuable when the formulation requires a continuous polyurethane structure with polybutadiene segments incorporated into the polymer network.
| Parameter | Mono-OH Liquid Polybutadiene | Di-OH Liquid Polybutadiene |
|---|
| Hydroxyl functionality | Mainly one OH group per chain | Two OH groups per chain |
| Role in polyurethane | Greater control over reactive contribution | More direct contribution to chain growth |
| Network contribution | More limited by functionality | Greater reactive connectivity |
| Main formulation variables | OH value, molecular weight, dosage | OH value, molecular weight, NCO/OH ratio |
| Typical design focus | Reactive modification and structural control | Polyurethane backbone and network formation |
How Functionality Changes Polyurethane Network Formation
The most important difference between mono-OH and di-OH liquid polybutadiene appears at the molecular level.
A polyurethane reaction depends on the reaction between hydroxyl groups and isocyanate groups. A molecule carrying two hydroxyl groups can connect with two isocyanate-containing species, allowing it to participate in chain extension or network formation. A molecule with only one hydroxyl group has a different connectivity and cannot provide the same two-ended growth mechanism.
This is why hydroxyl functionality should be evaluated before simply comparing product names or viscosities.
Consider two liquid polybutadiene grades with similar molecular weights. If one has mono-OH functionality and the other has di-OH functionality, the same mass of each material will not contribute the same number of reactive hydroxyl groups. The required amount of isocyanate must therefore be recalculated.
The difference becomes even more significant when the liquid polybutadiene represents a substantial portion of the polyol package. At higher loading levels, functionality can influence the balance between chain length, branching, network connectivity and unreacted groups.
In practical polyurethane development, the finished material should therefore be evaluated as a complete system rather than by the liquid rubber alone.
The NCO/OH Ratio Changes the Practical Result
When replacing one liquid polybutadiene grade with another, one of the first calculations should be the NCO/OH ratio.
The mass percentage of liquid polybutadiene does not tell you how much reactive hydroxyl functionality has entered the formulation. OH value or OH equivalent weight is much more useful because it allows the formulator to calculate the actual reactive equivalent.
A simple change from di-OH to mono-OH material can therefore require a meaningful reformulation even when the polymer backbone appears similar.
The practical sequence is:
Determine the hydroxyl equivalent contribution of the liquid polybutadiene.
Recalculate the total OH equivalents contributed by the complete polyol package.
Adjust the isocyanate amount according to the desired NCO/OH ratio or isocyanate index.
Recheck cure behavior and mechanical properties rather than assuming the original formulation remains chemically balanced.
This is particularly important when replacing an existing HTPB grade with a mono-OH liquid polybutadiene. Matching the nominal addition rate by weight can lead to a different NCO balance and therefore a different cured structure.
The correct comparison is based on reactive equivalents, not simply kilograms of product.
Molecular Weight Matters as Much as Hydroxyl Functionality
Functionality is only one part of the formulation equation. Molecular weight can be equally important.
Suppose two liquid polybutadiene products both have two hydroxyl groups per molecule. If their molecular weights are different, the number of molecules present at the same mass loading will also be different. This affects OH equivalent weight, viscosity, processing behavior and the spacing between reactive groups.
The same principle applies to mono-OH materials. A higher-molecular-weight mono-OH chain may introduce a relatively long polybutadiene segment while contributing only one reactive hydroxyl group.
For this reason, product selection should normally include at least:
hydroxyl value or OH equivalent weight
number-average or relevant molecular weight data
molecular-weight distribution where available
viscosity at a specified temperature
functionality and functionality distribution
unsaturation or structural information relevant to the intended chemistry
A supplier's viscosity value alone is not enough to establish that two grades are interchangeable.
Processing Behavior Can Decide Which Grade Works Better
Chemical functionality determines how a material can participate in polyurethane formation, but processing properties often determine whether that chemistry can be used efficiently on the production floor.
Viscosity and Mixing
Liquid polybutadiene can have a significant effect on the viscosity of a polyol blend. Higher viscosity can slow metering, mixing and degassing, particularly in systems processed at relatively low temperatures.
When comparing liquid polybutadiene for polyurethane, the relevant question is not only whether the material can react with the selected isocyanate. It is also whether the complete formulation can be mixed and processed consistently at production scale.
A formulation that performs well in a laboratory mixer may behave differently in a larger system if mixing time, shear rate, temperature and residence time change.
Dispersion and Compatibility
Polybutadiene is a nonpolar hydrocarbon-based structure, while many polyurethane formulations contain relatively polar components. Compatibility can therefore influence whether the final formulation remains homogeneous during mixing and curing.
The effect becomes especially important when other polyols, fillers, plasticizers, catalysts or reactive modifiers are present.
A grade that appears chemically suitable on paper may still produce poor dispersion or phase behavior if its molecular characteristics are poorly matched with the rest of the formulation. For that reason, compatibility should be evaluated under actual formulation conditions rather than inferred only from the polymer name.
Curing Behavior
Changing hydroxyl functionality changes the way the liquid polybutadiene contributes to the polyurethane reaction. Once the formulation is adjusted to the correct NCO/OH balance, the next question is how quickly and uniformly the system cures.
Catalyst concentration, temperature, moisture, isocyanate structure and other polyols can all affect reaction kinetics. The liquid polybutadiene should therefore be evaluated within the complete polyurethane formulation.
For production, pot life, demolding time, tack-free time and final cure development can be more useful than a simple laboratory reaction-rate comparison.
Which One Fits Flexible Polyurethane Formulations?
Both mono-OH and di-OH liquid polybutadiene can contribute to flexible polyurethane formulations, but they should not be selected solely because flexibility is the target property.
Flexibility is influenced by the polybutadiene segment, molecular weight, hard-segment content, crosslink density, isocyanate structure and cure conditions. A di-OH material can still produce a flexible polyurethane if the overall network density and formulation architecture are designed accordingly.
Likewise, a mono-OH material does not automatically guarantee a softer or more flexible product. Its lower functionality changes how it contributes to the network, but the final properties depend on the complete formulation.
For polyurethane elastomer development, the advanced polyurethane materials portfolio can be evaluated according to the required reactive functionality and application rather than treating all liquid polybutadiene grades as interchangeable.
A useful formulation approach is to start with the desired finished properties and work backward:
target properties → molecular architecture → functionality → OH equivalents → NCO/OH ratio → processing conditions
That approach is generally more reliable than starting with a fixed liquid-rubber loading and trying to adjust the formulation afterward.
What to Check Before Replacing One Liquid Polybutadiene Grade
A replacement should be treated as a formulation change, even when the supplier describes the new material as a comparable grade.
The first comparison should cover the basic chemical specifications, but the evaluation should not stop there. For industrial polyurethane production, consistency between batches can be just as important as the nominal specification.
Before approving an alternative grade, compare:
OH value and functionality: These determine the reactive-equivalent contribution.
Molecular weight and viscosity: These affect formulation concentration, mixing and processing.
Cured properties: Hardness, tensile strength, elongation, modulus, resilience and low-temperature behavior should be checked against the existing formulation.
The NCO/OH calculation should then be repeated using the actual specification of the replacement material.
For critical applications, laboratory screening should be followed by a production-scale trial. Small differences in viscosity, moisture, molecular-weight distribution or functionality can become more visible when the material is processed in larger batches.
Consistent raw-material quality is particularly important when the liquid polybutadiene is part of a repeatable polyurethane manufacturing process. Further's quality control system is therefore relevant when evaluating a supplier for applications where batch-to-batch consistency matters.
Mono-OH vs Di-OH Selection Should Start With the Finished Polyurethane
The most useful distinction between mono-OH vs di-OH liquid polybutadiene is not simply which one provides better mechanical properties. Their hydroxyl functionality determines how each material participates in polyurethane formation, while molecular weight and formulation balance determine how that difference appears in the finished product.
Mono-OH materials can be attractive when the formulation requires a controlled reactive contribution from a polybutadiene segment without the same two-ended connectivity provided by a di-OH polyol. Di-OH materials, by contrast, can contribute directly to polyurethane chain growth and network development.
The choice should therefore be based on the complete formulation rather than the liquid rubber in isolation. Functionality, OH equivalent weight, molecular weight, NCO/OH ratio, viscosity and cure conditions should be reviewed together before a grade is selected or replaced.
For formulators comparing different polybutadiene polyols, the key question is not “Which grade is stronger?” It is “How will this grade change the polyurethane structure at the required reactive-equivalent level?” That shift in evaluation usually leads to a more predictable formulation and a smoother scale-up from laboratory trials to production.
 English
 English
 Spanish
 Russian
 Arabic
 French
 German
 Portuguese
 Turkish
 Dutch
 Polish
 Korean
 Vietnamese
 Indonesian
 21. Jul, 2026