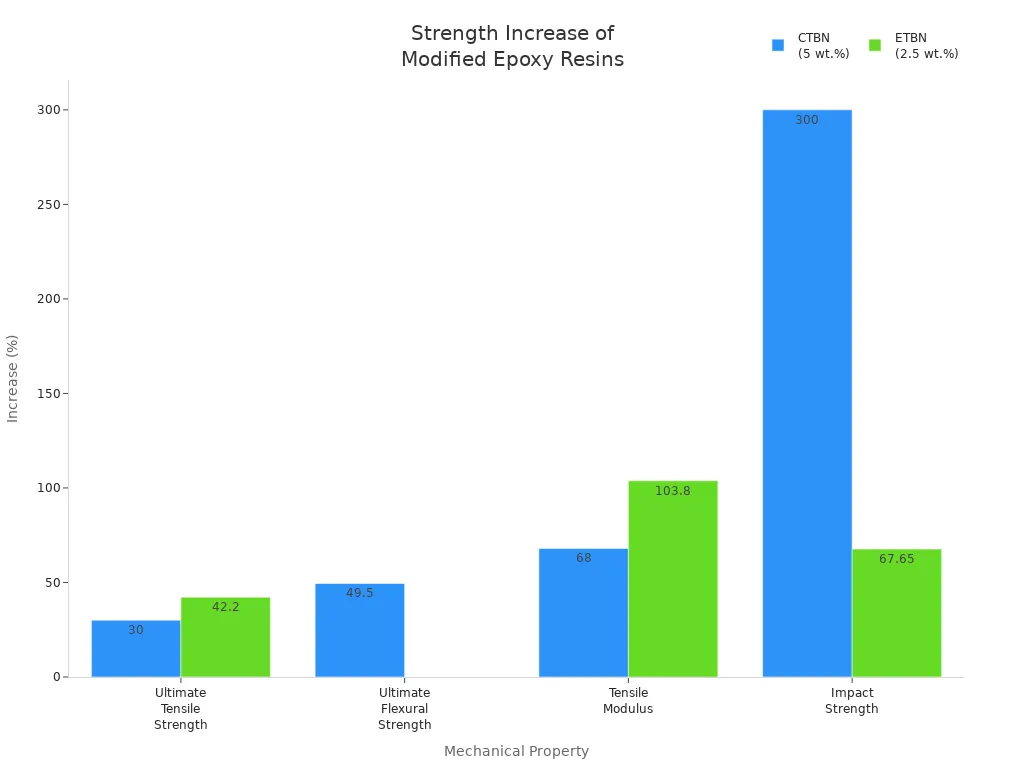
Why Epoxy Resins Need Reactive Toughening
Epoxy resins are widely used when a formulation needs high stiffness, dimensional stability, chemical resistance, adhesion, and thermal performance. The same highly crosslinked structure that provides these properties can also make cured epoxy relatively brittle, particularly when the material is exposed to impact, cyclic loading, thermal stress, or crack initiation at defects and interfaces.
Toughening an epoxy system is therefore a matter of changing how a material absorbs and distributes mechanical energy without sacrificing more of its original properties than the application can tolerate. Conventional plasticization can increase flexibility, but excessive plasticization may reduce modulus, heat resistance, and dimensional stability. Rubber modification takes a different approach by introducing flexible segments or a dispersed elastomeric phase capable of absorbing energy during deformation.
Epoxy functionalized polybutadiene is particularly interesting because it combines the flexible polybutadiene backbone with epoxy functionality. The polybutadiene portion provides low-temperature flexibility and rubber-like molecular mobility, while the epoxy groups can interact chemically with the surrounding resin or curing system. This makes the material relevant to reactive toughening of epoxy resin, where the modifier is designed to become more closely integrated with the cured network rather than acting solely as a physically blended rubber.
The formulation objective is not simply to add as much flexible material as possible. The more useful goal is controlled modification of the epoxy network, including the balance between toughness, modulus, glass transition temperature, viscosity, cure behavior, and phase morphology.
What Makes Epoxy Functionalized Polybutadiene Different
Flexible Polybutadiene Backbone
The polybutadiene backbone provides a flexible hydrocarbon structure with relatively high chain mobility. When incorporated into an epoxy formulation, these segments can introduce molecular flexibility that is not present to the same extent in a rigid thermoset network.
This flexibility can contribute to higher elongation and improved energy dissipation. In a toughened epoxy, the rubber phase can deform under applied stress and help reduce the tendency of a crack to propagate directly through the brittle matrix.
The effect depends strongly on molecular weight. A lower-molecular-weight material may be easier to blend and process, while a higher-molecular-weight grade can provide longer flexible segments but may increase formulation viscosity. Molecular weight should therefore be considered together with functionality and target loading rather than treated as an isolated specification.
Epoxy Functionality and Chemical Reactivity
The defining difference between a conventional liquid polybutadiene and an epoxy-functional grade is the presence of reactive epoxy groups.
These groups can provide chemical interaction with the epoxy formulation during curing. Depending on the specific molecular architecture and curing chemistry, the functionalized polybutadiene can become incorporated into the network or establish stronger chemical connections between the rubber-rich phase and the surrounding epoxy matrix.
That distinction matters because a rubber phase with poor interfacial bonding can become a defect under load. Stronger chemical interaction can improve stress transfer between the flexible phase and the rigid matrix, although the actual result remains dependent on resin chemistry, curing agent, functionality, and processing conditions.
Epoxy Functionalized vs Epoxy Terminated Polybutadiene
The terms epoxy-functionalized polybutadiene, epoxy-terminated polybutadiene, and epoxidized polybutadiene are related but should not automatically be treated as identical materials.
The location and concentration of epoxy groups influence how the modifier interacts with the resin network. Epoxy functionality distributed along the polybutadiene backbone can produce a different reaction pattern from a material whose reactive groups are concentrated at the chain ends.
Material type | Functional group characteristics | Potential formulation role |
Epoxidized polybutadiene | Epoxy groups introduced through modification of PB unsaturation | Reactive modification and changes in polarity and compatibility |
Epoxy-terminated polybutadiene | Reactive epoxy groups concentrated at chain ends | Network incorporation through terminal functionality |
Hydroxyl-terminated polybutadiene | Hydroxyl groups at chain ends | Reactive flexible component, particularly in polyurethane chemistry |
Non-functional liquid polybutadiene | No intentionally reactive terminal functionality | Primarily physical modification and flexible-phase formation |
For formulation development, the actual technical specification is more important than the generic material name. Epoxy value, equivalent weight, molecular weight, functionality, viscosity, and compatibility should all be considered before selecting a grade.
How Epoxy Functionalized Polybutadiene Interacts With the Epoxy Network
Chemical Incorporation During Cure
The performance of a reactive liquid rubber depends partly on what happens to its functional groups during curing.
When epoxy-functionalized polybutadiene participates in the curing process, part of the modifier can become chemically associated with the developing thermoset network. This can reduce the likelihood of a completely unbound rubber phase and may improve stress transfer across the rubber-matrix interface.
The exact reaction mechanism depends on the epoxy resin and curing agent. Amine-cured, anhydride-cured, and other epoxy systems can respond differently to the same reactive modifier. For this reason, a supplier's material specification cannot replace formulation-level compatibility and cure testing.
Interfacial Adhesion Between Rubber and Epoxy
Interfacial adhesion is one of the key factors separating useful rubber toughening from simple plasticization.
If the rubber-rich phase has adequate interaction with the epoxy matrix, mechanical stress can be transferred into the flexible domains, allowing them to deform and dissipate energy. If adhesion is weak, the interface may debond prematurely and become a source of crack initiation.
Epoxy functionality can help address this problem by increasing chemical interaction between the modifier and the resin network. The resulting performance still depends on the degree of reaction, functional-group concentration, phase size, and curing conditions.
The Role of Epoxy Group Location
Functional-group location is not merely a chemical detail. It can influence network structure and the distribution of flexible segments within the cured resin.
Research on epoxy-functional polybutadiene systems has shown that the structure and position of oxirane functionality can affect curing behavior as well as the thermal and mechanical properties of the resulting epoxy material.
For practical formulation work, this means two materials with similar polybutadiene content may not provide equivalent results if their epoxy functionality and molecular architecture are different.
Compatibility and Phase Morphology in Modified Epoxy Resin
Dissolved Rubber vs Phase-Separated Rubber
A reactive liquid rubber does not necessarily remain uniformly molecularly dissolved throughout the entire curing process. As the epoxy network develops, the thermodynamic balance of the system changes. The modifier may remain compatible with the resin at one stage and subsequently form a separate rubber-rich phase as molecular weight and network density increase.
Controlled phase separation can be beneficial for toughening. A finely dispersed rubber phase can act as an energy-dissipating region while the epoxy remains the continuous structural phase.
Uncontrolled phase separation is a different situation. Large rubber domains, poor dispersion, or weak interfaces can create stress concentrations and reduce tensile or thermal performance.
Rubber Particle Size and Distribution
The size and distribution of rubber-rich domains influence how cracks interact with the modified epoxy.
A well-dispersed morphology can provide multiple sites for energy dissipation as a crack moves through the material. Large agglomerates, by contrast, can behave as defects rather than toughening structures.
This is why the same liquid rubber modifier can produce different results at different concentrations or under different cure schedules. Mixing temperature, shear history, resin viscosity, curing kinetics, and modifier compatibility can all affect the morphology established before the network becomes fully crosslinked.
Why Interfacial Adhesion Matters
Morphology and interfacial chemistry cannot be evaluated independently.
A small rubber domain with weak adhesion may debond too easily. A larger domain with strong interfacial bonding may behave differently under fracture. The useful morphology is therefore determined by the combination of domain size, distribution, rubber stiffness, matrix properties, and interface strength.
For development work, microscopy or other morphology analysis is most useful when correlated with fracture toughness, impact strength, tensile properties, and dynamic mechanical analysis rather than considered as a standalone result.
How Epoxy Functionalized Polybutadiene Changes Resin Performance
The expected property changes depend on molecular structure, modifier concentration, curing chemistry, and morphology. There is no universal performance direction for every property.
Performance parameter | Potential effect of reactive polybutadiene | Main variables |
Fracture toughness | Potential increase | Rubber morphology, loading, interfacial adhesion |
Elongation | Generally increased | Flexible-chain content and network structure |
Impact resistance | Potential improvement | Rubber-phase size and energy dissipation |
Tensile strength | May decrease at excessive loading | Network dilution and phase morphology |
Modulus | May decrease | Flexible-phase concentration |
Glass transition temperature | May decrease | Rubber content and crosslink density |
Adhesion | Potential improvement | Chemical interaction and interface quality |
Viscosity | Can increase or decrease depending on grade and loading | Molecular weight, temperature, formulation composition |
The important point is that epoxy resin toughening involves trade-offs. Increasing the amount of flexible material may improve elongation while reducing stiffness. A stronger rubber contribution may improve fracture resistance while lowering Tg. Higher molecular weight may provide useful chain behavior while making mixing more difficult.
Formulation development therefore needs a defined target property profile rather than a single optimization target such as maximum impact strength.
How Loading Level Affects Epoxy Functionalized Polybutadiene Performance
Low Loading and Network Modification
At relatively low loading, epoxy-functionalized polybutadiene may primarily modify the local network structure and introduce flexible segments without producing a large, clearly separated rubber phase.
This approach can be useful when the formulation needs a moderate increase in flexibility or crack resistance while retaining much of the original epoxy's stiffness and thermal performance.
The magnitude of the effect depends on the reactive functionality of the modifier and the extent to which it becomes incorporated into the curing network.
Moderate Loading and Rubber-Phase Toughening
As the modifier concentration increases, phase separation may become more pronounced during curing. The resulting dispersed rubber phase can provide a more obvious toughening mechanism.
At this stage, particle size and distribution become increasingly important. A formulation can show a significant improvement in fracture behavior when the rubber phase is sufficiently fine and well bonded to the matrix.
This is also where formulation screening becomes essential. The optimum loading for one epoxy resin should not automatically be transferred to another because resin functionality, curing agent, stoichiometry, and processing conditions can change the final morphology.
Excessive Loading and Property Trade-Offs
Beyond the useful formulation window, additional rubber does not necessarily produce additional toughness.
High modifier concentrations can reduce crosslink density, increase the amount of flexible phase, raise viscosity, and promote larger or more interconnected rubber-rich domains. These changes may reduce modulus, Tg, tensile strength, or dimensional stability.
Studies of reactive liquid-rubber-modified epoxy systems have reported increases in elongation alongside reductions in tensile strength or Tg at higher modifier contents, illustrating why loading must be optimized as part of the complete formulation rather than on the basis of toughness alone.
Processing and Curing Considerations
Viscosity and Mixing
The processing characteristics of the modifier can be just as important as its cured-state properties.
A higher-molecular-weight polybutadiene generally contributes more strongly to formulation viscosity. If viscosity becomes too high, dispersion, filler incorporation, degassing, coating application, or casting can become more difficult.
Temperature can be used to manage viscosity during mixing, but excessive heating may also affect cure kinetics or storage stability. Production-scale processing should therefore be evaluated under conditions representative of the intended manufacturing process.
Useful processing parameters include:
· viscosity at the actual mixing temperature;
· addition sequence;
· mixing shear and duration;
· dispersion stability;
· filler compatibility;
· degassing behavior;
· pot life and storage stability.
Epoxy Value and Equivalent Weight
For reactive epoxy-functional materials, epoxy value and epoxy equivalent weight are important formulation parameters because they provide information about the concentration of reactive epoxy functionality.
These values should be considered when calculating formulation stoichiometry. Treating the modifier only as a percentage of total resin can lead to an incomplete understanding of its contribution to the curing reaction.
The relevant calculation depends on the product specification and the curing system, so formulation engineers should use the supplier's verified analytical values rather than assume a theoretical functionality from the material name.
Curing Agent Compatibility
A reactive modifier needs to be compatible not only with the base epoxy resin but also with the curing agent.
Changes in reaction kinetics can influence gelation, phase separation, network development, and final morphology. A modifier that reacts too slowly or too quickly relative to the surrounding resin can produce a different structure from the one expected from simple blending.
For this reason, formulation screening should include cure behavior rather than relying exclusively on final mechanical testing.
Cure Temperature and Phase Development
Temperature influences both chemical reaction rates and phase behavior. During heating, the epoxy network becomes progressively more crosslinked while the compatibility of the rubber-rich component with the developing network can change.
The final morphology is therefore partly a consequence of the curing path.
Two formulations with identical ingredients can produce different properties if they use different mixing temperatures, cure schedules, post-cure conditions, or processing times. This is particularly important when moving from laboratory batches to production equipment.
Where Epoxy Functionalized Polybutadiene Fits in Resin Formulations
Structural Adhesives
Structural adhesives require a combination of adhesion, toughness, fatigue resistance, and dimensional stability. A rigid epoxy network can provide strong cohesive performance, while a reactive rubber phase can help dissipate energy around defects and crack tips.
The value of epoxy-functionalized polybutadiene in such systems depends on maintaining sufficient cohesive strength while introducing enough flexible-phase behavior to improve fracture resistance.
Protective and Functional Coatings
Epoxy coatings are often selected for chemical resistance, adhesion, hardness, and durability. Excessive flexibility can compromise hardness or abrasion resistance, but insufficient toughness can leave a cured coating vulnerable to cracking under impact or substrate movement.
A reactive liquid rubber can provide a way to modify the network while maintaining a stronger connection with the epoxy matrix than a purely non-reactive plasticizer.
Electrical and Electronic Encapsulation
Thermoset materials used in electrical and electronic applications can experience thermal cycling and mechanical stress caused by differences in thermal expansion between the resin and embedded components.
Here, the formulation challenge is particularly demanding because improvements in toughness or flexibility must be balanced against electrical insulation, thermal stability, dimensional control, and processing requirements.
For manufacturers developing epoxy resin applications, reactive liquid-rubber selection should therefore be evaluated alongside the complete resin, filler, curing-agent, and processing package.
Composite and Thermoset Systems
Epoxy matrices used in composites and other engineered thermosets often need high stiffness combined with resistance to crack initiation and propagation. Reactive rubber modification can be considered when fracture behavior becomes a limiting property.
The most useful approach is to evaluate the modified resin as a complete matrix system, including reinforcement compatibility, viscosity, wet-out behavior, curing, and final interfacial performance.
Key Parameters for Selecting an Epoxy Functionalized Polybutadiene
Material selection should start with the formulation requirements rather than with a single product specification. The following parameters are particularly relevant during supplier evaluation and laboratory screening:
· Molecular weight — influences viscosity, chain mobility, and the behavior of the flexible phase.
· Molecular-weight distribution — can affect processing consistency and formulation rheology.
· Epoxy value — indicates the level of reactive epoxy functionality.
· Epoxy equivalent weight — important for stoichiometric formulation calculations.
· Functionality — influences how the modifier can interact with the developing epoxy network.
· Viscosity — affects mixing, dispensing, coating, casting, and filler incorporation.
· Degree of functionalization — affects polarity, reactivity, and interaction with the epoxy matrix.
· Resin compatibility — influences dispersion and phase morphology.
· Curing-agent compatibility — affects reaction kinetics and final network structure.
· Thermal stability — relevant to cure temperature, post-cure, and service conditions.
· Batch consistency — essential for repeatable formulation performance.
For procurement teams, a complete technical data sheet is only the starting point. Application testing should confirm that the selected grade behaves consistently with the specific epoxy resin, curing agent, filler package, and processing conditions used in production.
Formulation Development Should Start With the Epoxy Network
The role of epoxy functionalized polybutadiene is best understood through the structure of the complete cured system.
The polybutadiene backbone introduces flexible molecular segments. Epoxy functionality provides a route toward chemical interaction with the resin network. Molecular weight affects viscosity and chain mobility. Loading controls the amount and structure of the rubber-rich phase. Compatibility and cure kinetics determine how that phase develops. Interfacial adhesion then influences whether the resulting morphology can effectively dissipate mechanical energy.
These variables are closely connected. Changing the modifier concentration can change morphology; changing morphology can change fracture behavior; changing functionality can alter curing; and changing molecular weight can affect both processing and final network structure.
For that reason, selecting an epoxy-functional liquid rubber should not begin with the question of which grade provides the highest reported toughness. A more useful formulation approach starts with the required balance of fracture resistance, modulus, Tg, viscosity, cure behavior, adhesion, and thermal stability, then identifies the molecular structure and functionality capable of achieving that balance.
That approach gives epoxy-functionalized polybutadiene a defined role within the resin formulation rather than treating it as a generic rubber additive.
 English
 English
 Spanish
 Russian
 Arabic
 French
 German
 Portuguese
 Turkish
 Dutch
 Polish
 Korean
 Vietnamese
 Indonesian
 04. Aug, 2026